Hi this is Team Merchant Navy Decoded !!!

Please fill the below form with your query and we will get back to you in next 12 hours.

Rest assured your data is safe with us !!!🙂

Ask Your Query

Marine Boiler Burners

Marine Boiler Burners

Ask a boiler operator what fails most often on the auxiliary boiler, and mostly, the answer comes back to the burner. Not the shell, not the tubes, the burner. A dripping atomizer tip, a cracked quarl, a scanner that’s stopped seeing the flame properly. It’s a small assembly compared to the boiler sitting around it, but it does the one job everything else depends on: taking thick, stubborn fuel oil and turning it into something that’ll actually burn cleanly.

And here’s the thing  there isn’t just one design. Walk onto three different ships and you might find three different burner types doing that same job in three genuinely different ways. So let’s get into how each one is actually built, not just what it does in theory.

Types of Burners

Types of Burners

Marine residual fuel oil, straight out of the tank, is nowhere near ready to burn well. It’s viscous, it doesn’t vaporize evenly, and if you just squirt it into a furnace as a stream it’ll smoke and soot up everything in sight. Before it even reaches the burner it gets preheated usually somewhere around 90–120°C for the heavier grades  to bring the viscosity down into a workable range. Get that preheat wrong in either direction and atomization suffers: too cold and the droplets come out too big, too hot and the spray gets uneven right at the tip.

Once it’s at the right viscosity, the burner’s job is to atomize it, break it into a fine mist, tens to low hundreds of microns across  and mix that mist with the right amount of swirling combustion air. How that atomization actually happens is where the three main types genuinely part ways.

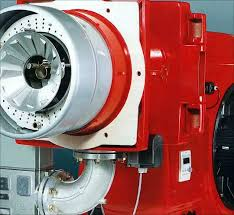
Pressure Jet Burners: The Simple One

This is the design most people picture when they think “burner,” mostly because it’s mechanically the simplest of the three. There’s no separate atomizing medium here; the fuel oil itself does the work, forced through the tip under pressure, typically somewhere in the 7–15 bar range, sometimes higher on certain designs.

How it’s built:–

  • Oil travels down a central lance to the burner tip
  • At the tip,it hits a swirl plate – A small disc machined with angled slots or grooves that force the oil into a spinning motion. 
  • Right behind that sits the orifice (or sprayer) plate, a precisely sized hole the swirling oil is forced through.
  •  The combination of spin plus pressure drop across that tiny orifice is what shreds the oil into a fine, hollow-cone spray as it exits. 
  • Some designs add a spring-loaded piston behind the tip  as fuel pressure rises, the piston pulls a spindle back, opening up the swirl chamber and uncovering extra ports, which helps keep atomization quality reasonably consistent across a wider range of firing rates than a fixed orifice ever could manage on its own.

The catch: Atomization quality is entirely tied to oil pressure. Drop the pressure too low  which happens naturally at low firing rates  and the spray falls apart, droplets get coarse, and you get incomplete combustion. That’s why pressure jet burners typically only manage a turndown ratio (the range between minimum and maximum stable firing rate) of around 3.5:1, sometimes worse. Fewer moving parts, less to maintain, but a narrower operating window.

Uses:-

  • Smaller auxiliary boilers and package boilers running at a fairly steady load
  • Boilers where mechanical simplicity and low maintenance matter more than a wide firing range
  • Land-based and industrial boiler plant, where the same design is common outside shipping too
  • Applications where the load doesn’t swing much, so the narrow turndown isn’t a real limitation day to day

Table of Contents

Steam (and Air) Atomizing Burners : Letting Something Else Do the Shredding

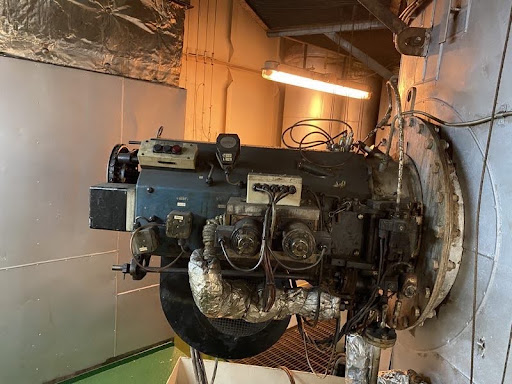
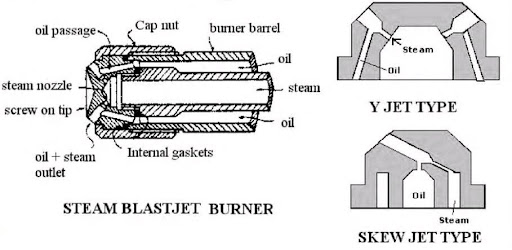
This is the design that’s dominated marine Scotch boilers for well over a century, and for a decent reason: Instead of relying on oil pressure alone to atomize, it uses a separate jet of steam (or sometimes compressed air) to physically tear the oil apart at the tip. That means atomization quality doesn’t collapse just because oil flow is low  the steam keeps doing its job regardless.

Construction comes in two basic ways:-

  • External mix – Steam and fuel stay completely separate right up until they leave the burner tip. Fuel goes to a standard pressure-tip atomizer while steam flows around the outside of the fuel passage and exits through an annular gap, given a swirl angle that roughly matches the fuel spray. At low fuel pressure, the steam (held at a constant supply pressure through the whole turndown range) does most of the atomizing work; at higher fuel pressure, the pressure tip itself starts contributing more. No mixing happens inside the burner body at all; it’s all happening in open air right at the exit.
  • Internal mix – Steam and fuel are actually brought together and mixed into an emulsion inside the burner, then expanded together through the discharge holes. The two most common internal-mix designs are the “Y-jet” and the “skew jet.” This approach tends to be more tolerant of viscosity swings and is generally frugal with steam consumption, which matters more than you’d think on a boiler that’s already burning fuel to make the steam it’s using to atomize more fuel.

One practical downside worth knowing: Without that steam or air flow constantly cooling the tip, the burner has to be pulled out of a lit boiler when it’s not firing otherwise residual heat will carbonize fuel sitting in the tip and clog it solid.

Uses:-

  • Scotch marine boilers, where this design has been the traditional standard for over a century
  • Exhaust gas economiser boilers and composite boilers that need to follow main engine load changes smoothly
  • Cargo ships and tankers running a boiler across a genuinely wide range of steam demand, from port to full sea passage
  • Installations where a long, well-proven track record matters more than avoiding the extra steam or air consumption atomizing requires

Rotary Cup Burners: Spinning the Problem Away

Rotary Cup Burners

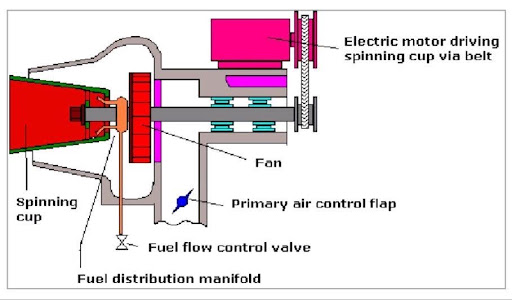
This one looks and works completely differently from the other two. Instead of pressure or a jet of steam, it uses a small, high-speed motor-driven cup to fling the oil apart through centrifugal force.

How it’s built :-

  •  Low-pressure fuel oil flows into a conical cup rotating at high speed (driven by an electric motor through a belt and pulley arrangement in a lot of designs). 
  • The oil spreads out as a thin, even film across the inside of the cup and gets thrown off the rim as it spins  essentially the same principle as flicking water off a spinning bicycle wheel, just far more controlled. 
  • That thrown-off film is still fairly coarse on its own, which is where primary air comes in: a dedicated primary air fan blasts high-velocity air concentrically around the cup rim, striking that oil film at speed and shattering it down into genuinely fine droplets, creating an evenly mixed air-fuel mist right at the source. 

Primary air typically makes up a fairly small slice of the total combustion air; commonly cited figures put it around 7%, with the remaining 93% arriving as secondary air through the wind box and air register, directed into the flame by adjustable vanes.

Because atomization here depends on cup speed and primary air rather than fuel pressure, rotary cup burners handle low firing rates far more gracefully than a pure pressure jet design turndown ratios of 4:1 or better are typical, and they’re comparatively insensitive to viscosity swings, meaning they don’t demand quite as tight a control on fuel preheat. The trade-off is more moving parts (a cup, a drive motor, bearings, a belt or direct drive) and correspondingly more to maintain. Ignition on these is usually handled by a separate diesel oil igniter lance inserted through the wind box and air register, which gets automatically purged with air once the burner’s established and the igniter’s no longer needed.

Uses:-

  • Boilers that spend real time running at low load rather than mostly at full firing rate
  • Vessels with frequent, wide load swings, where a burner needs to ride those changes out without constant restarting
  • Installations where tight control over fuel preheat is difficult to guarantee, since rotary cup tolerates viscosity swings better than the other two types
  • Larger boiler plant where the extra moving parts (cup, motor, drive) are an acceptable trade for that operating flexibility

Pilot & Main Burner

Every one of the three designs above shares one detail :None of them lights the main heavy fuel spray directly with a spark.

Why not? A spark igniter can light easily vaporized diesel oil without much trouble. Heavy fuel oil, even properly preheated, is  far harder to ignite reliably straight off a spark. So every burner arrangement uses a two-stage ignition sequence instead: a small pilot burner lights first, and the pilot’s flame is what actually lights the main burner.

STAGE 

What Happens

1. Purge

Forced draft fan runs to clear any unburnt fuel vapour from the furnace before any ignition attempt

2. Pilot ignition

A small diesel oil pilot burner is sparked alight  diesel ignites far more reliably than heavy fuel

3. Flame proving

The flame scanner (photocell) confirms the pilot flame is actually established and stable

4. Main fuel admitted

Only once the pilot flame is proven does the burner management system (BMS) open the main fuel valve

5. Main flame established

The heavy fuel spray ignites from the pilot flame, and the scanner shifts to confirming the main flame


What happens to the pilot after that depends on the design:-

  • Interrupted pilot – The pilot shuts off once the main flame is proven stable, since it’s no longer needed and continuously burning diesel oil alongside the main flame would be wasteful
  • Continuous pilot – The pilot keeps burning throughout firing, acting as a constant backup ignition source, at the cost of extra diesel oil consumption

Either way, the safety logic is the same: no proven pilot flame means no main fuel valve opening, ever. This is the same flame-scanner-and-BMS interlock covered further down, just applied one stage earlier in the sequence  proving the pilot before proving the main flame, rather than only checking for a flame once fuel is already flowing.

This is also exactly what’s happening with the rotary cup burner’s diesel igniter lance mentioned above. It’s not a separate concept, it’s the same pilot-then-main logic, just implemented as a physical lance inserted through the wind box rather than a fixed pilot nozzle.

If a pilot flame fails to establish within a set trial-for-ignition period, the BMS aborts the whole start attempt and re-purges the furnace before allowing another try  it doesn’t just keep sparking indefinitely into an unlit furnace.

A Quick Side-by-Side

Type

What atomizes the fuel

Typical turndown

Fuel preheat sensitivity

Moving parts

Pressure jet

Oil pressure through swirl/orifice plate

3.5:1

High–narrow tolerance

Fewest

Steam/air atomizing

Separate steam or air jet at the tip

6:1 or better

Moderate

Few

Rotary cup

Spinning cup + primary air shear

4:1 or better

Lower – more tolerant

Most (cup, motor, drive)

What’s Common to All Three

Whichever atomizing method is doing the work, everything downstream looks fairly similar. The atomized spray meets secondary combustion air delivered through a wind box and shaped by an adjustable air register – Vanes or a damper that controls both the volume and the swirl of the air. That mixture ignites, usually via a pilot flame or spark igniter running easier-to-light diesel oil rather than heavy fuel, and the whole flame is stabilized at its root by the quarl –  A refractory-lined, typically conical throat that reflects heat back into the flame base and shapes the early flame envelope. A flame scanner (photocell, UV, or IR) watches continuously, and the burner management system won’t allow fuel to keep flowing if that scanner loses sight of the flame.

Where Things Tend to Go Wrong

Loss of fuel preheat shows up as smoke and poor combustion on pressure jet and steam-atomizing burners alike, since both rely on viscosity being within a fairly tight window. Worn swirl or orifice plates degrade spray pattern gradually and get replaced on a schedule rather than run to failure. Low fuel supply pressure on a pressure jet burner can let fuel drip into the furnace instead of atomizing properly, a genuinely dangerous setup, since that unburned fuel can accumulate and ignite all at once. On rotary cup burners, worn cup bearings or a slipping drive belt show up as poor atomization even when everything else checks out fine. And across all three types, a spalled quarl, a fouled scanner, or sooted heat transfer surfaces downstream are the classic signs something upstream at the burner has been drifting out of adjustment for a while.

Conclusion

Three different mechanisms, one shared goal: take fuel that cannot burn cleanly on its own, and force it  through pressure, through steam shear, or through raw centrifugal spin  into droplets fine enough to actually combust properly. Pressure jet wins on simplicity, steam atomizing wins on turndown and a long, proven track record, rotary cup wins on tolerance for low loads and preheat variation. None of them is universally “the right one” it comes down to what the boiler was designed around and how the ship actually operates it.

Frequently Asked Questions (FAQs)

It’s too viscous to form fine droplets unaided. Without atomization — by pressure, steam/air shear, or centrifugal spin  it burns incompletely and you end up with soot, smoke, and poor heat transfer.

Depends entirely on the boiler and how it’s run. Pressure jet if you want mechanical simplicity, steam-atomizing if you want a wide, well-proven turndown range, rotary cup if the boiler needs to run comfortably at low loads without babying the preheat.

It’s the spread between a burner’s max and min stable firing rate. Wider turndown means the boiler can follow load changes without constantly stopping and restarting the burner, which is both more efficient and easier on the ignition components.


Without steam or air flow cooling the tip, residual furnace heat will carbonize any fuel left sitting in the passages and clog it. Pulling the burner out of a lit boiler avoids that.


The flame scanner, tied into the burner management system. Loss of a confirmed flame signal trips the fuel supply immediately, regardless of which atomizing method the burner uses.

Disclaimer :- The opinions expressed in this article belong solely to the author and may not necessarily reflect those of Merchant Navy Decoded. We cannot guarantee the accuracy of the information provided and disclaim any responsibility for it. Data and visuals used are sourced from publicly available information and may not be authenticated by any regulatory body. Reviews and comments appearing on our blogs represent the opinions of individuals and do not necessarily reflect the views of Merchant Navy Decoded. We are not responsible for any loss or damage resulting from reliance on these reviews or comments.

Reproduction, copying, sharing, or use of the article or images in any form is strictly prohibited without prior permission from both the author and Merchant Navy Decoded.

DIWALI SALE

Decoded Discount Alert! up to 50% OFF

DIWALI SALE

Decoded Discount Alert! up to 50% OFF

Use Coupon Code Deep50

Days
Hours
Seconds
0
Would love your thoughts, please comment.x
()
x